

Hangzhou QMS Medical Co., Ltd. is a professional manufacturer specializing in medical ventilators, ICU ventilation systems, and respiratory care equipment for healthcare institutions worldwide. Established in 2015, the company is located in Hangzhou, China, a city recognized for its strong medical technology and advanced manufacturing industries.
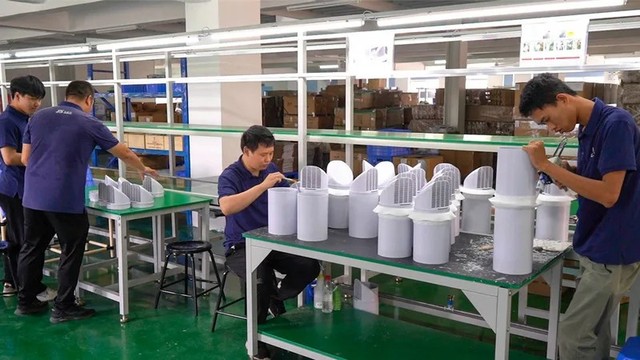
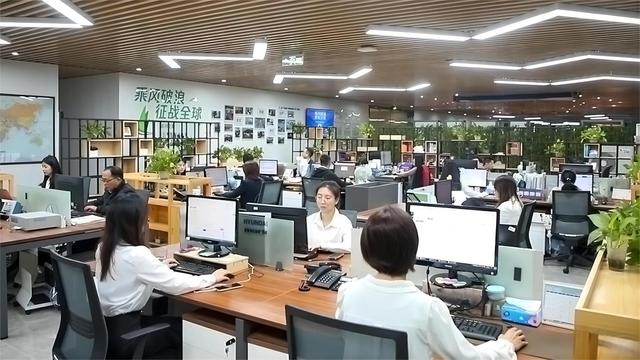
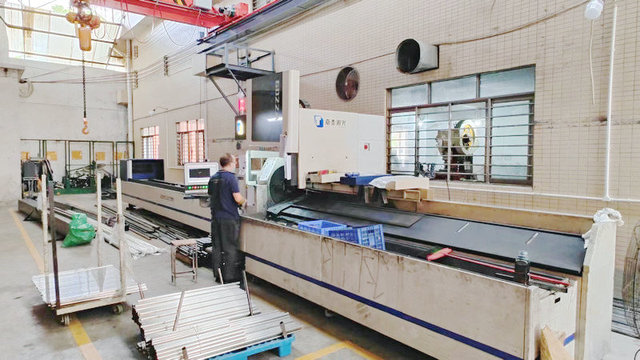
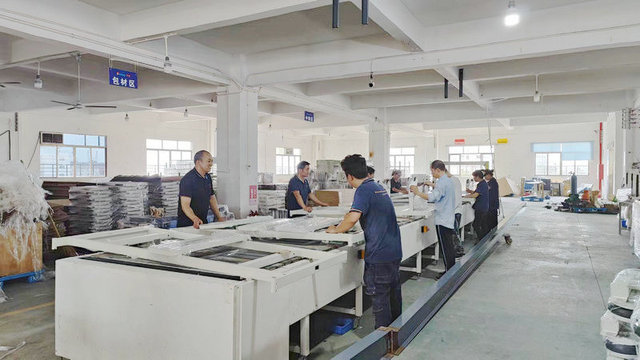
The company operates a modern production facility covering approximately 10,000 square meters and employs more than 220 skilled professionals, including engineers, technicians, and quality management specialists. QMS Medical focuses on the research, development, production, and supply of respiratory support technologies designed for hospitals, intensive care units, emergency departments, ambulance services, and home healthcare applications.
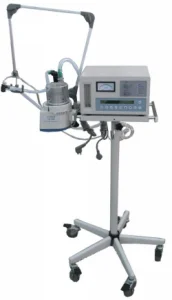
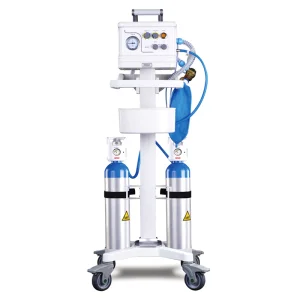
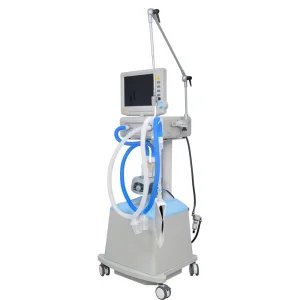
Its product portfolio includes ICU ventilators, portable ventilators, transport ventilators, emergency respiratory support systems, non-invasive ventilation devices, and intelligent patient monitoring integration solutions. The company continuously invests in product innovation and engineering development to improve ventilation performance, operational reliability, and clinical usability across diverse healthcare environments.
Supported by a dedicated R&D team and advanced manufacturing capabilities, QMS Medical implements comprehensive quality management procedures throughout product design, component sourcing, assembly, testing, and final inspection. The company is committed to delivering respiratory care solutions that support healthcare professionals in managing critical and long-term respiratory conditions.
Serving customers across Europe, North America, Asia, the Middle East, Africa, and Latin America, Hangzhou QMS Medical Co., Ltd. provides flexible OEM and ODM manufacturing services to meet different market requirements. Through continuous technological advancement and customer-focused development, the company aims to contribute to the global healthcare industry by providing reliable, efficient, and innovative respiratory care equipment for modern medical applications.
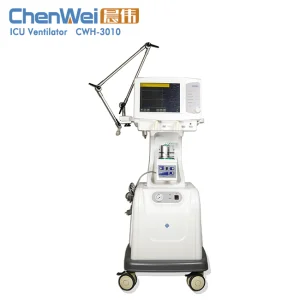


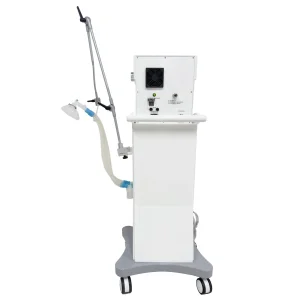
The global landscape of hospital infrastructure is undergoing a seismic paradigm shift driven by digital transformation, precision medicine, and strict regulatory requirements. Modern healthcare facilities demand clinical ecosystems capable of seamless interoperability, real-time patient monitoring data integration, and absolute structural resilience. As a leading OEM/ODM factory and supplier, Hangzhou QMS Medical Co., Ltd. sits at the intersection of clinical engineering and smart manufacturing, providing scalable solutions designed to meet the rigorous demands of 21st-century healthcare systems.
Looking toward the future, the integration of Artificial Intelligence (AI) and Internet of Medical Things (IoMT) into hospital ventilation and critical care infrastructure is no longer optional—it is a core necessity. Predictive maintenance algorithms, automated airflow optimization, and remote diagnostic capabilities are redefining how critical care units operate. Our roadmap focuses on embedding edge-computing capabilities directly into our ICU and transport ventilators, ensuring clinicians receive actionable physiological insights instantly while maintaining fail-safe mechanical redundancy.
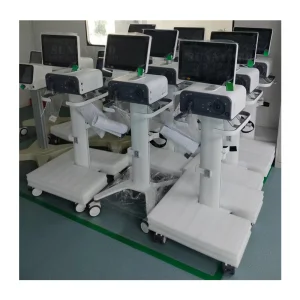
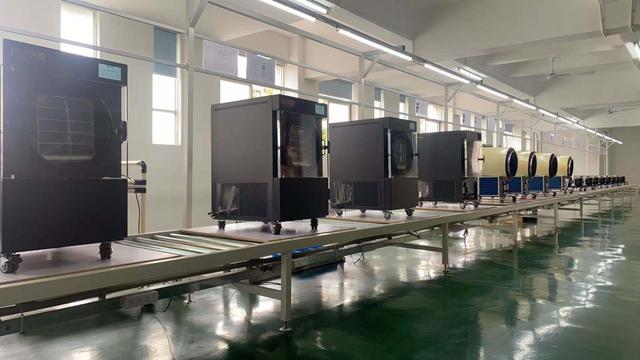
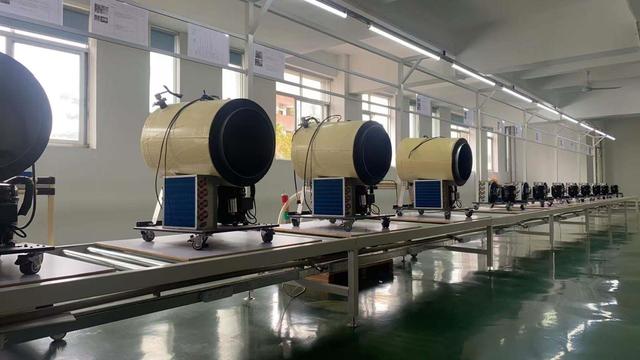
Operating out of Hangzhou—a recognized global hub for technological innovation—QMS Medical leverages the immense advantages of China's Industry 4.0 manufacturing framework. Our 10,000-square-meter facility utilizes automated precision assembly lines, robotic calibration stations, and rigorous computer-integrated manufacturing (CIM) systems to eliminate human error and achieve unprecedented production scalability.
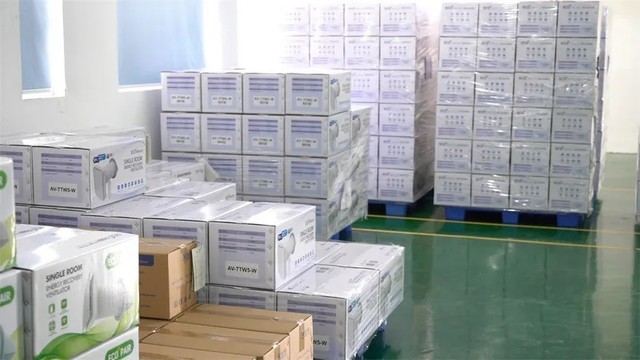
Supply chain resilience is anchored in our localized yet globally compliant sourcing strategy. By establishing robust tier-1 supplier networks for specialized medical-grade sensors, pneumatic valves, and biocompatible polymers, we insulate our manufacturing pipeline from external bottlenecks. This structural resilience guarantees stable lead times, transparent quality control logs, and cost-effective OEM/ODM pricing models for international procurement managers.
International hospital groups, government health ministries, and medical device distributors face complex procurement challenges ranging from cross-border regulatory hurdles to customized localization demands. QMS Medical provides comprehensive macro-level industry solutions, assisting partners from initial architectural layout consultation to turnkey equipment deployment.
Whether outfitting a metropolitan tertiary care hospital's new intensive care wing or supplying portable emergency ventilation units for regional ambulance fleets, our engineering consultants collaborate directly with biomedical procurement committees. We offer modular configuration options, multi-language operating interfaces, and adaptable power supply specifications to ensure frictionless deployment across diverse geographic and economic landscapes.
Our manufacturing processes strictly adhere to ISO 13485, CE certification standards, and FDA manufacturing guidelines, ensuring absolute legal and clinical compliance in target export markets across Europe, North America, and beyond.
We provide comprehensive after-sales support, including remote diagnostic firmware updates, modular spare parts availability, and biomedical engineering training programs to maximize equipment uptime in critical care settings.
From custom branding and proprietary software UI skins to bespoke mechanical casing designs, our engineering team works as an extension of your R&D department to bring unique medical products to market swiftly.
As a direct manufacturer, QMS Medical offers flexible MOQ structures tailored to our partners' market entry strategies. For standard catalog items, low initial batches are supported, while custom OEM/ODM projects are evaluated based on tooling, software customization, and component sourcing specifications.
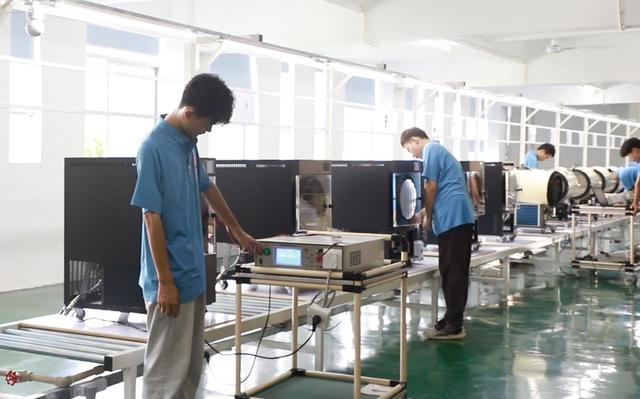
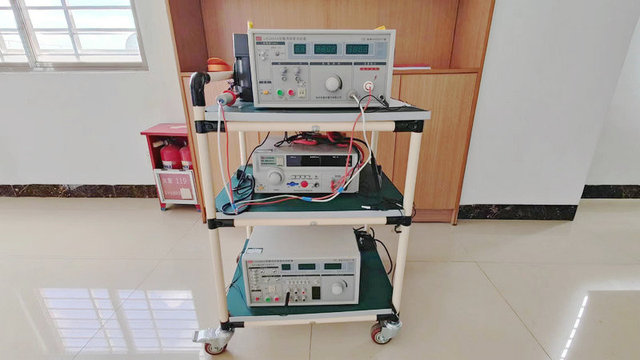
Our quality assurance protocol encompasses four critical stages: incoming raw material inspection (IQC), in-process assembly monitoring (IPQC), 100% full-load aging and performance testing of finished ventilators (FQC), and pre-shipment auditing (OQC) compliant with international medical device standards.
Our products are manufactured under strict ISO 13485 quality management systems. Major ventilator lines and clinical support systems carry CE certifications and meet major international electrical safety and respiratory performance benchmarks.
Yes. Our dedicated software and hardware R&D teams specialize in custom firmware development, multi-language UI localization, and specialized ventilation mode programming to satisfy distinct clinical protocols across global health sectors.
 QMS Medical